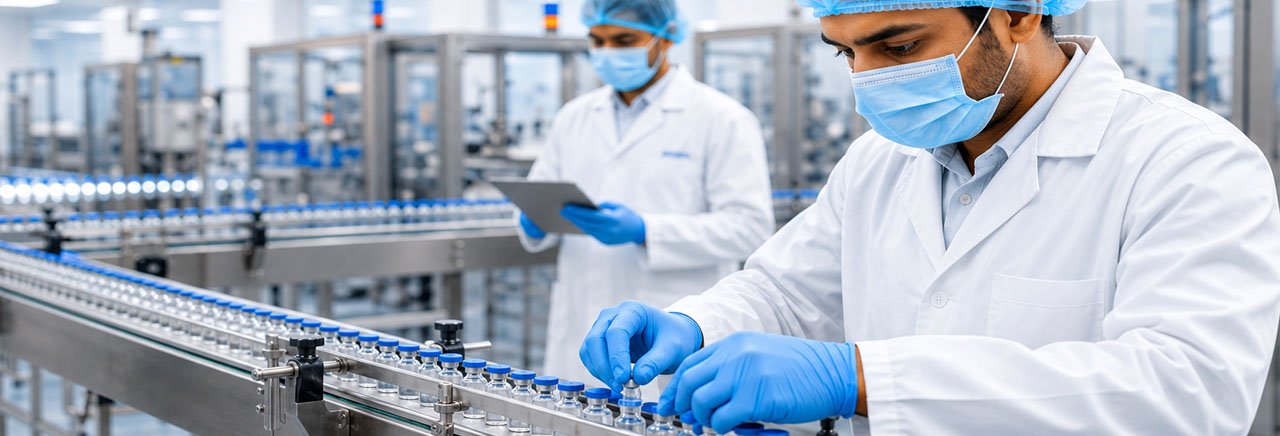
We follow stringent quality standards and advanced manufacturing processes to deliver safe, effective and reliable healthcare products.
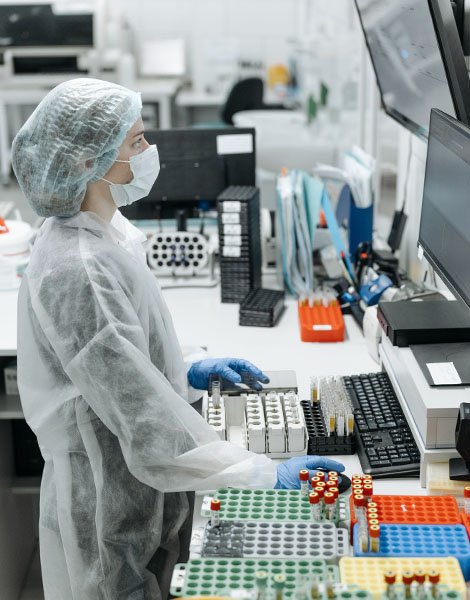
Quality and precision are at the heart of our manufacturing processes. Our production facilities operate with advanced technology and follow strict regulatory standards to ensure that every product meets the highest levels of safety, purity, and effectiveness.
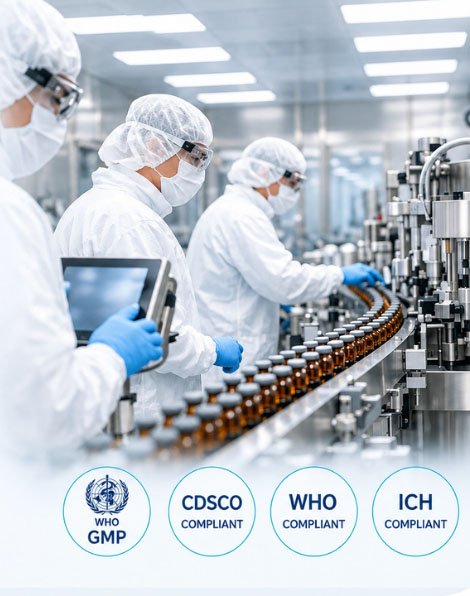
Contract manufacturing at WHO-GMP certified facilities.
Units with modern technology (Alu-Alu blister, HDPE jars, dry syrup filling).
Fully automated & controlled environments.
Compliance with Indian (CDSCO), WHO, and ICH guidelines.
Raw material sourcing from approved vendors only.
100% batch testing: assay, dissolution, uniformity, microbial load.
Stability testing (accelerated & real-time).
Packaging integrity checks to avoid counterfeiting.
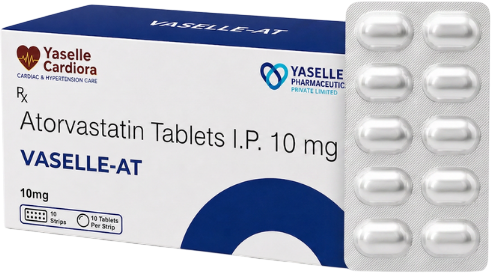
Alu-Alu / blister packs for enhanced stability.
Patient-friendly packs (10’s, 15’s, 30’s).
Tamper-evident seals & barcoding.
Designed to differentiate against competitor packs.
WHO-GMP, ISO 9001:2015 certified facilities.
Regular audits for Good Laboratory Practices (GLP).
DPCO/NPPA compliance for price-regulated molecules.
Commitment to sustainable & eco-friendly operations.
We are committed to improving lives through quality pharmaceutical products, innovation, and reliable healthcare solutions. Our focus remains on safety, effectiveness, and patient well-being.
Copyright © 2026 YasellaPharma. All Rights Reserved.